Industrial processes depend on efficient pumps to transfer water, chemicals, oils, acids, alkalis and other liquids safely. Choosing a reliable Centrifugal Pump Manufacturer is important for maintaining continuous operations, reducing breakdowns and improving fluid-handling performance.
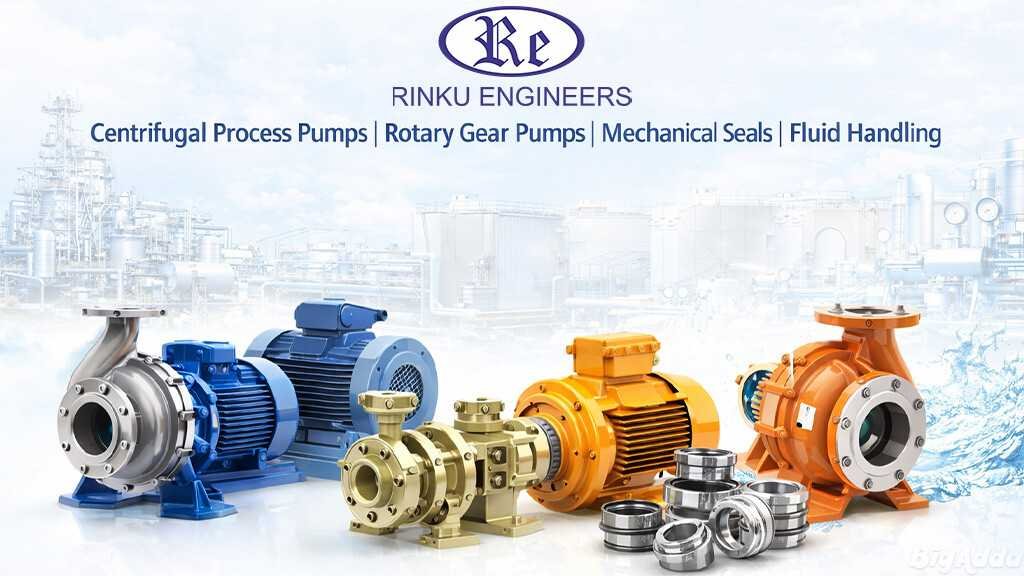
Rinku Engineers manufactures AYUSH pumps for chemical, pharmaceutical, textile, food-processing, water-treatment and other process industries. Its product range includes centrifugal process pumps, chemical pumps, rotary gear pumps, lobe pumps, sewage pumps and mechanical seals.
What Is a Centrifugal Process Pump?
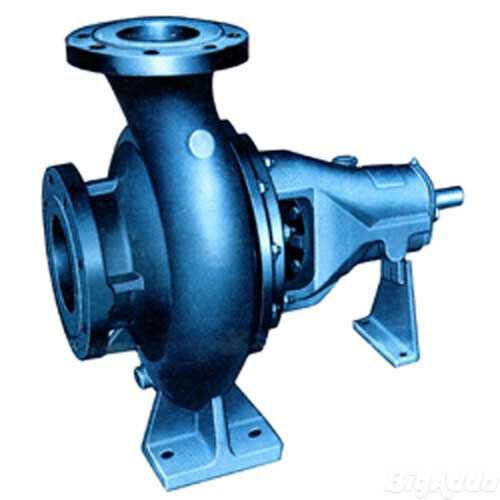
A centrifugal process pump transfers liquid by converting rotational energy into fluid movement. The rotating impeller moves the liquid through the pump and creates the pressure required for transfer.
These pumps are widely used because they provide smooth flow, simple operation and dependable performance. The correct pump selection depends on the liquid, required flow rate, pressure, temperature and operating environment.
Industrial Applications of Centrifugal Pumps
Centrifugal pumps are used across several industries for transferring different types of liquids. Common applications include:
- Chemical transfer and processing
- Pharmaceutical manufacturing
- Water-treatment systems
- Food and edible-oil processing
- Textile-processing plants
- Sludge and slurry handling
- Hydrocarbon transfer
- Filter press applications
- Sewage and wastewater handling
- General industrial water circulation
Each application requires a pump with suitable materials, sealing arrangements and operating specifications.
Industrial Pumps Offered by Rinku Engineers
Rinku Engineers provides different pumps for varied fluid-handling requirements.
Polypropylene Pumps
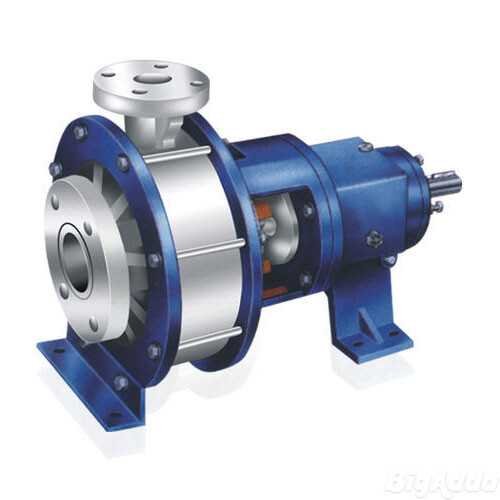
Polypropylene pumps are suitable for transferring corrosive chemicals, acids and alkalis. Their corrosion-resistant construction makes them useful in chemical-processing applications.
Multistage Feed Pumps
Multistage feed pumps use multiple impellers to generate higher pressure. They are suitable for applications requiring increased head and steady liquid delivery.
Chemical Process Pumps
Chemical process pumps are designed for transferring industrial chemicals and process liquids. Pump materials and sealing systems should be selected according to the chemical properties.
Self-Priming Pumps
Self-priming pumps can evacuate air from the suction line and begin pumping without repeated manual priming. They are useful where the liquid source is below the pump level.
Air-Cooled Pumps
Air-cooled pumps are designed for applications where a separate cooling-water arrangement may not be convenient. They support fluid transfer under specific process conditions.
Sewage Submersible Pumps
Sewage submersible pumps operate while submerged in the liquid. They are used for wastewater, sewage and drainage applications.
Slurry-Handling Pumps
Slurry-handling pumps are designed to transfer liquids containing suspended solids. They are useful in demanding industrial processes involving mud, sludge or slurry.
Rotary Gear and Lobe Pumps
Rotary gear pumps and lobe pumps are commonly selected for oils, viscous liquids and controlled fluid transfer. Their positive displacement operation supports consistent delivery.
Importance of Mechanical Seals
Mechanical seals help prevent leakage where the rotating pump shaft passes through the pump casing. Selecting the correct seal can improve safety, reduce liquid loss and protect surrounding equipment.
Rinku Engineers offers multi-spring seals, single-coiled seals, bellow seals and double mechanical seals for different pumps and operating conditions.
How to Select the Correct Industrial Pump
Before choosing an industrial pump, provide the manufacturer with complete application information. Important details include:
- Required flow rate
- Total operating head
- Liquid name and composition
- Temperature and viscosity
- Specific gravity
- Presence of solids
- Suction conditions
- Material compatibility
- Required motor capacity
- Preferred sealing arrangement
This information helps the manufacturer recommend a pump suitable for the process.
Why Choose an Experienced Pump Manufacturer?
An experienced Pump Manufacturer can help identify the correct pump type, construction material and seal arrangement. Proper selection can improve performance, reduce maintenance and extend equipment life.
Rinku Engineers has over 25 years of experience in industrial pumping and sealing systems. The company focuses on cost-effective products, timely delivery and after-sales support for industrial customers.
Conclusion
Selecting a suitable centrifugal pump is essential for safe and efficient liquid handling. Businesses should consider the liquid properties, flow rate, head, temperature, construction material and sealing system before purchasing a pump.
Rinku Engineers offers a broad range of AYUSH pumps and mechanical seals for different industrial applications. Visit Rinku Engineers to explore available products and submit your operating requirements for a quotation.